ROVEMA UK has completed the installation of an advanced sugar packaging solution for British Sugar, supporting the modernisation of its production operations. The flexible, high-performance brick pack system handles multiple product formats while overcoming significant site access and installation challenges.
Each packaging project brings a distinct set of operational demands. For British Sugar, the priority was to introduce a versatile solution capable of producing several retail sugar formats while delivering outstanding pack quality, production efficiency and dependable long-term operation.
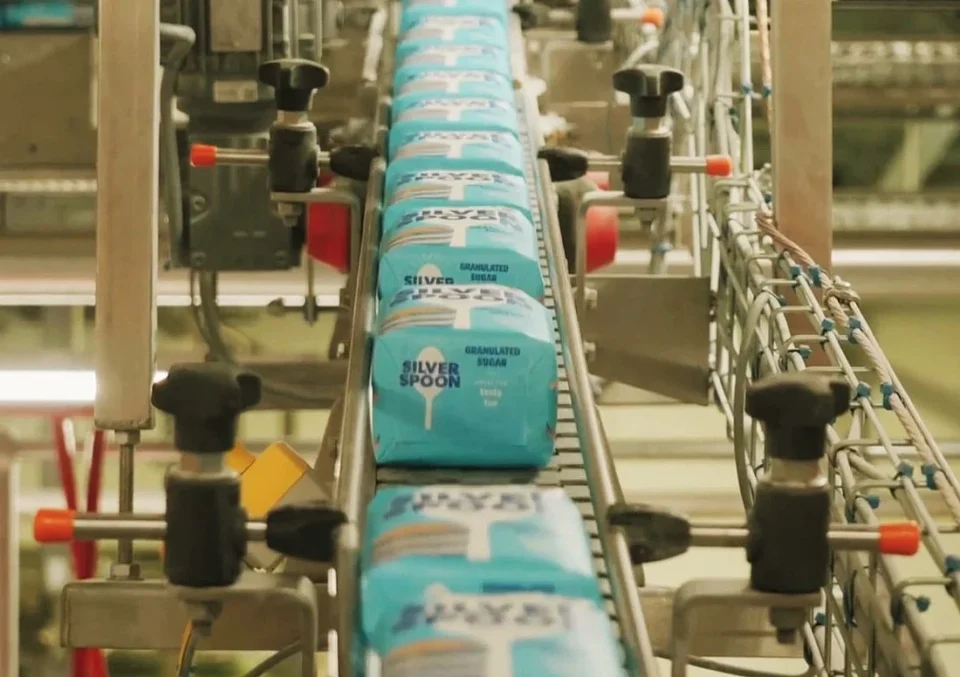
In partnership with British Sugar’s team, ROVEMA UK supplied and commissioned SBS Single Tube and SBS Twin Tube brick pack systems. Together, the machines provide a flexible production platform for packing sugar products from 500g to 2kg in fully recyclable, shelf-ready brick packs.
Engineering That Goes Beyond Equipment Supply
The project highlighted the importance of engineering expertise throughout the installation process, not only in the design and supply of the machinery. A major challenge arose before production could begin.
Because the packaging equipment had to be installed on a second-floor production level, limited site access ruled out conventional delivery and installation methods. ROVEMA engineers responded by modifying the machines for transportation in two sections. Each section was carefully lifted into position, reassembled and commissioned on-site.
This approach meant British Sugar did not need to compromise its production plans to accommodate the equipment. ROVEMA preserved the intended machine design and performance while meeting the site’s specific installation requirements, demonstrating a practical and customer-led approach to packaging engineering.
One Platform for Multiple Sugar Formats
Installed within British Sugar’s packing facility, the SBS Single Tube and SBS Twin Tube systems provide the flexibility to manufacture a broad selection of sugar products on the same line.
The ROVEMA SBS platform combines Vertical Form Fill and Seal (VFFS) technology with dedicated downstream modules. This integrated process produces compact, stackable brick packs efficiently and consistently.
Although the system is widely used for powder applications, its capabilities extend across food and non-food markets. More than 350 SBS installations are currently operating worldwide, demonstrating the platform’s broad application range and relevance to evolving food manufacturing trends.
Its modular construction supports every stage of production, including bag forming, precise dosing, sealing and final pack shaping. As a result, manufacturers can maintain consistent pack quality across different product weights and formats while responding to changing food and beverage industry trends.
On the British Sugar application, the SBS Twin Tube system achieves outputs of up to 100 bags per minute. Depending on the product characteristics and pack specifications, the wider SBS platform can operate at speeds of up to 160 bags per minute.
The SBS Single Tube machine works alongside the twin-tube system to provide further production versatility. It delivers the same high standards of accuracy, pack integrity and operational reliability before transferring completed packs to the downstream palletising system.
Accurate Dosing for Reliable Pack Quality
A ROVEMA SDH Servo Auger Doser is installed above each packaging machine to provide precise product filling at high production speeds.
Servo-controlled auger technology regulates the quantity of sugar delivered to each pack, supporting accurate and repeatable filling performance.
Product is continuously mixed inside the hopper to maintain a consistent flow. The gentle filling process also helps reduce dust generation, supporting clean seals, dependable pack weights and stable production performance. This level of control reflects the wider role of food processing technology in improving efficiency and quality across modern packaging operations.
A Partnership Built for Long-Term Performance
Since commissioning, British Sugar has achieved production rates above expectations on selected pack formats. The results demonstrate the value of combining advanced packaging equipment with close collaboration and effective project management.
For ROVEMA, the installation reinforces the company’s belief that every packaging project must be designed around the customer’s specific operational goals. Whether the requirement involves overcoming complex access restrictions, integrating specialist dosing equipment or preparing a line for future capacity needs, the objective remains consistent: to provide efficient, dependable packaging performance over the long term.
Alex Spain, Marketing Manager at ROVEMA UK, commented:
“Every customer has different production requirements, and that’s why collaboration is such an important part of every project we undertake. This installation demonstrates that our job is so much more than simply supplying a packaging machine. We need to understand each application, overcome any engineering challenges, and deliver a tailored solution that continues to perform for many years. We’re delighted to have supported British Sugar with this project and look forward to continuing our strong partnership.”
Manufacturers seeking to improve packaging efficiency, expand format flexibility or upgrade existing production lines can rely on ROVEMA UK for complete packaging support. Its services cover product trials, system design, equipment installation, commissioning and ongoing lifecycle assistance. The approach also supports wider priorities shaping food and drink industry innovation, including food and drink sustainability, evolving food and drink regulations, advances in food and drink packaging, changing food and drink marketing requirements and emerging food and drink consumer trends.